 Buyer reference
Plan the audit around the equipment you are buying.
An equipment factory audit should be built around the specific machines in the quotation, not around the showroom. For a rig purchase, the audit covers four areas: machining and fabrication capability, assembly of the actual unit, the test bay where load and pressure ratings are proven, and the quality documents behind the certificates. Each area produces evidence that can be checked later, so the visit should be documented with photos and records rather than impressions.
Before the visit, send the audit agenda and ask for the manufacturing schedule of your model. If your unit is in production, the visit can follow the actual build stages: machining, welding, assembly, test. If the factory builds to order, ask to see a completed unit of the same class and the test records from its delivery.
Step 1: Check the machining and fabrication capacity.
Oilfield equipment is judged on the machining that produces the load-bearing parts. Walk the machining shops and note the machine types: CNC lathes and boring machines for drawworks drums and sheaves, gear cutting capability for transmissions, and weld fabrication for masts and substructures. The age and condition of the machines matter less than whether the parts in your quotation are made in-house or bought out; for bought-out parts, ask where they are made and request the quality records. A factory that machines the critical components itself controls the tolerances and the traceability; one that only assembles bought-out parts depends entirely on its suppliers.
Step 2: Follow the assembly of the actual unit.
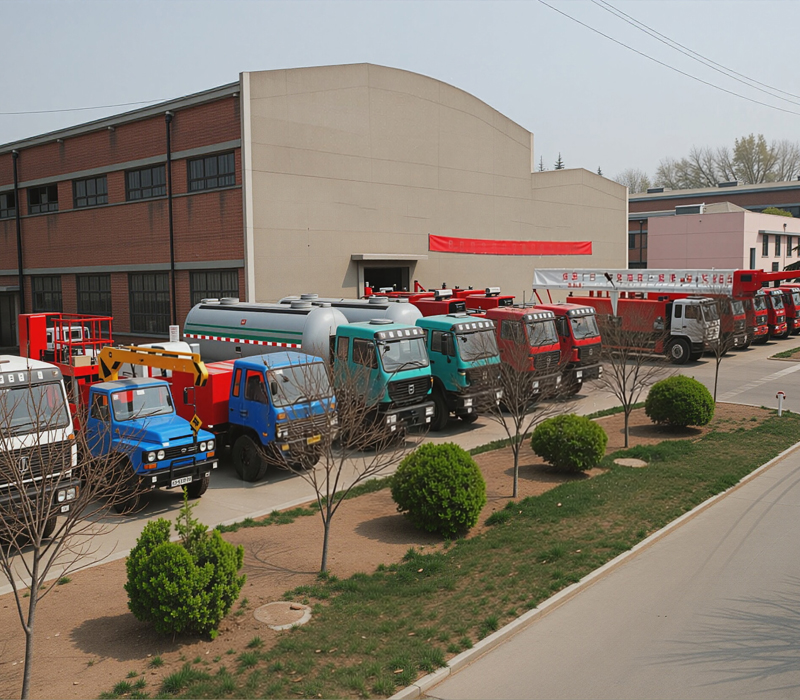
Ask to see the unit of your class in the assembly bay. Check the work in progress: whether the mast and substructure welds are clean and consistent, whether the drawworks and transmission are assembled with torque-controlled fasteners, whether wiring and hydraulics are routed and labeled, and whether the assembly area has the fixtures and lifting capacity for the size of equipment quoted. A working assembly bay with a rig of the same class in progress is the strongest evidence that the factory builds what it quotes. A sales office with no workshop behind it is the opposite signal.
Step 3: Verify the test bay and the test records.
Every rig quotation carries load, pressure and speed ratings. The test bay is where those ratings are proven: a load test on the mast and hoisting system, a pressure test on the pumps and manifolds, and an operating test on the drives. Ask for the test records of the last completed unit of your class — the test report dates, the loads reached, the witness signatures — and compare them with the certificate scope. If the factory cannot show test records for the model quoted, treat the ratings as design figures until they are proven.
Step 4: Audit the quality documents and the certificate scope.
Request the quality system certificates and the API license scope, and check two points specifically: that the certificates name the plant you are standing in (a group-level certificate from another plant is a common mismatch), and that the API product specifications cover the models quoted. The certificate verification method is covered in the API certifications guide in this resources section. For the quality system, ask how the plant handles non-conformance: where defects are logged, how they are corrected, and whether the corrective records survive an audit. A plant that keeps its non-conformance records open for inspection is easier to trust than one that shows only the awards wall.
Step 5: Watch for the common warning signs.
- Certificates or licenses naming a plant different from the one visited.
- No test records for the model quoted, or records without dates and signatures.
- Critical parts bought out without supplier quality records.
- Assembly work in progress without routing or inspection documents.
- A sales and export office with no visible workshop, or a workshop that cannot show a unit of the quoted class.
- Pressure and load ratings quoted without a test basis.
Remote audit as a first step.
When a physical visit is not possible before the order, run a video audit as a first step: a live walkthrough of the workshop and test bay, copies of the quality documents and the API license scope, and — if your unit is in production — a live load or pressure test witnessed over video. Keep the recorded material as part of the order file. A remote audit does not fully replace an on-site visit for critical equipment, but it filters the candidates before you commit travel and budget.
What to take from the visit.
Write the audit into the quotation conversation: ask the supplier to confirm which machining is in-house, which parts are bought out, how the test records will be delivered with the unit, and whether a factory inspection is included in the delivery schedule. A factory that supports a structured audit is easier to work with through commissioning and after-sales, because the same discipline shows up in the documentation and the spares support.